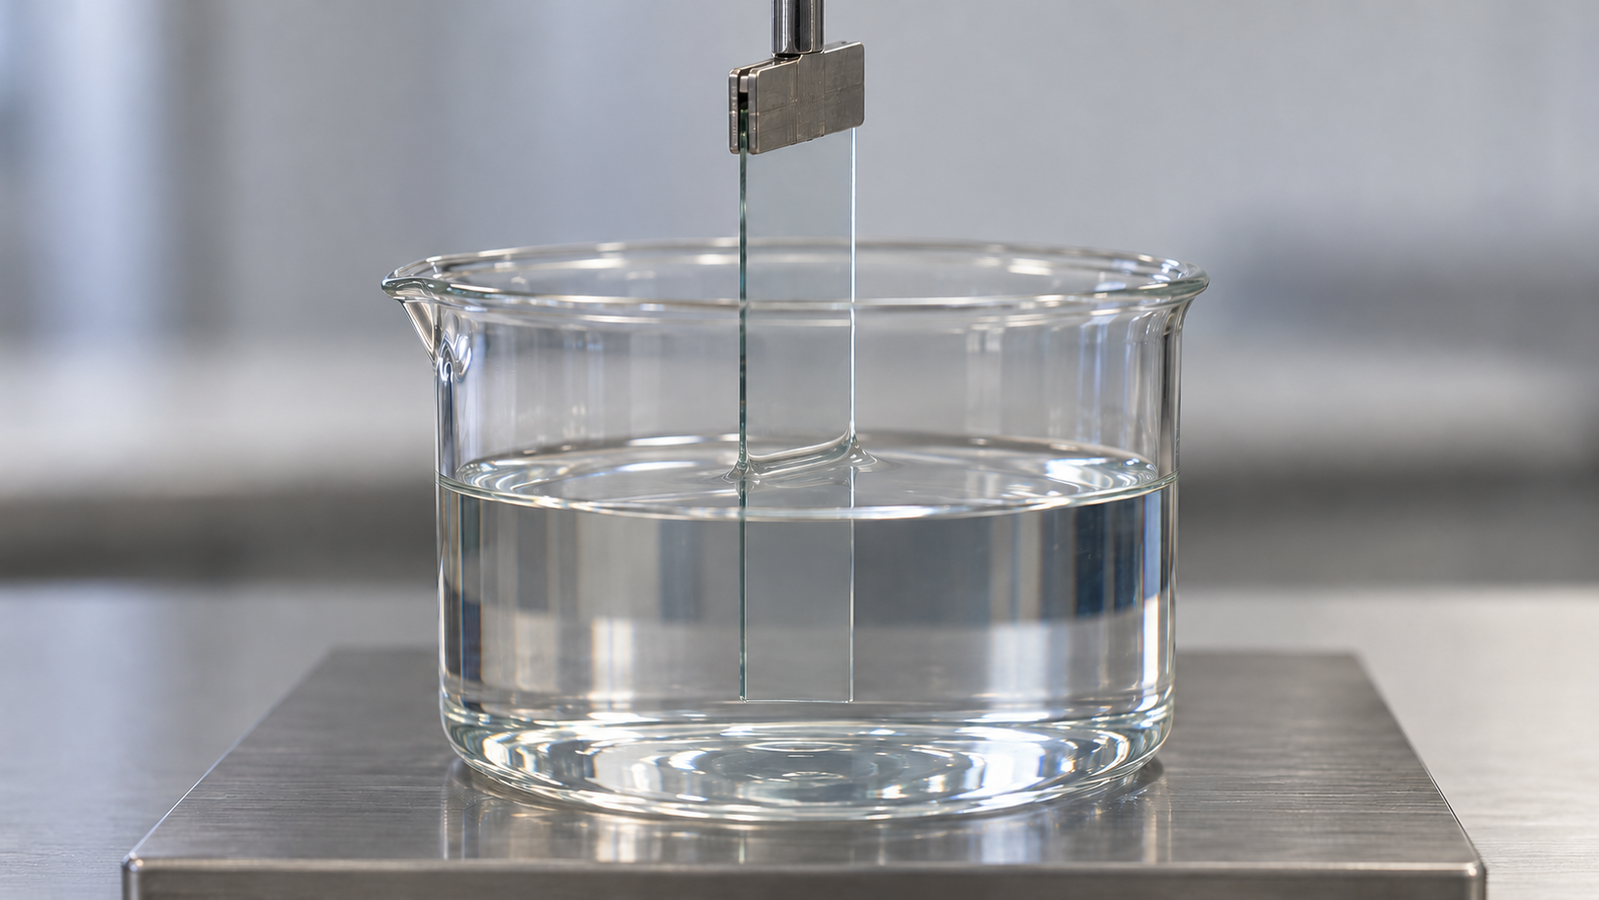
A heated dip coater adds one more control to the usual list of withdrawal speed, solution and atmosphere: temperature. Warming the bath or the substrate changes three liquid properties at once. The solvent evaporates faster, the viscosity falls and the surface tension drops slightly. Which of these dominates depends on the coating regime. This guide explains how temperature moves the capillary and draining branches of the thickness–speed curve, where the thickness minimum goes, what a heated base does and does not tell you about the liquid temperature, and how to plan a temperature series you can trust.
In one paragraph: in the capillary regime at very low speeds, thickness is set mainly by how fast solvent evaporates at the meniscus, so a warmer liquid usually gives a thicker film at the same speed. In the draining regime at higher speeds, thickness follows viscosity, so a warmer, thinner liquid usually gives a thinner wet film. Both effects push the thickness minimum to a higher withdrawal speed. The set-point of a heated base is not the temperature of the liquid at the meniscus, so measure the bath temperature, let it settle and run a speed series at each temperature.
1. The short answer
Five points cover most decisions about heating in dip coating:
- Temperature acts through liquid properties. Evaporation rate, viscosity and, to a lesser extent, surface tension all change with temperature, and each enters the thickness laws differently [1][2].
- In the capillary regime, warmer usually means thicker. Thickness there scales with the evaporation rate divided by the withdrawal speed, so faster evaporation deposits more material per unit length [3].
- In the draining regime, warmer usually means thinner wet films, because the entrained thickness rises with viscosity to the power 2/3 and viscosity falls on heating [4].
- The minimum moves to higher speed. Both effects shift the speed at which the thickness is lowest, so a speed that sat on one branch at room temperature may sit on the other when heated.
- Set-point is not liquid temperature. Measure the bath, allow it to settle, keep the atmosphere the same and run a full speed series at each temperature.
If dip coating regimes are new to you, start with the companion guide Dip Coating Explained: Withdrawal Speed, Coating Regimes and Film Thickness. For where dip coating fits among solution coating methods, see the pillar guide to solution-processed thin films.
2. What temperature changes in the liquid
Heating a coating solution changes several properties together. It is rarely possible to change one without the others, which is why a temperature series needs careful interpretation.
| Property | Usual direction on heating | Where it enters dip coating |
|---|---|---|
| Solvent vapour pressure | Rises steeply (Clausius–Clapeyron behaviour) | Drives the evaporation rate at the meniscus and on the wet film |
| Evaporation rate | Usually rises, also set by airflow and vapour above the bath | Capillary-regime thickness; drying time of the wet film |
| Viscosity | Falls for most liquids | Draining-regime thickness, roughly as viscosity2/3 |
| Surface tension | Falls slightly | Draining-regime thickness, weakly (power −1/6); wetting and meniscus shape |
| Density | Falls slightly | Draining-regime thickness, weakly (power −1/2) |
| Reaction and ageing rate | Usually rises for reactive sols | Sol stability over a session; viscosity drift |
| Solute solubility | System-dependent | Precipitation or crystallisation at the meniscus |
Qualitative trends for typical solvent-based coating liquids. Actual values depend on the solvent, solute and concentration; measure or look up the properties of your own liquid at its working temperature.
The strongest of these effects is usually the vapour pressure. The Clausius–Clapeyron relation, and empirical fits such as the Antoine equation, describe how the vapour pressure of a pure liquid rises roughly exponentially with temperature. The evaporation rate does not follow vapour pressure exactly, because it also depends on how quickly vapour is carried away from the surface, but in still air at a fixed geometry a warmer liquid generally evaporates faster. Viscosity changes are often smaller in relative terms, and surface tension and density change only slightly over a few tens of kelvin.
3. A quick recap of the two regimes
The thickness of a dip-coated film depends on withdrawal speed in two distinct ways [2][3]:
- Draining regime (higher speeds). The moving substrate drags a liquid film out of the bath, and viscous drag balances gravity and capillary forces at the meniscus. For a Newtonian liquid at low capillary number, the Landau–Levich relation gives a wet thickness hwet ≈ 0.94 (ηU)2/3 / (γ1/6(ρg)1/2), where η is viscosity, U withdrawal speed, γ surface tension, ρ density and g gravitational acceleration [4][5]. The film dries after it has formed, and the dry thickness is roughly the wet thickness times the volume fraction of non-volatile material.
- Capillary regime (very low speeds). The substrate moves so slowly that solvent evaporates at the meniscus faster than a draining film can form. Solute is fed to the contact line by capillary flow and deposits there. Thickness rises as speed falls, approximately in proportion to the evaporation rate divided by speed [3][6].
For the final dry thickness h, a working form following Faustini and co-workers adds the two contributions: h ≈ A/U + B·U2/3, where A grows with the evaporation rate and the solute content, and B collects the draining-regime terms together with the conversion from wet to dry thickness [3][2]. The sum has a minimum at an intermediate speed. In practice A and B are fitted to a measured thickness–speed series rather than calculated from first principles. Numerical studies of the evaporative regime reproduce the same general picture while showing that the details depend on the drying conditions near the meniscus [7].
4. Temperature in the capillary regime
In the capillary regime, the deposited thickness depends on how much solute reaches the contact line per unit time compared with how quickly the substrate moves away. Evaporation at the meniscus drives the capillary flow that carries solute there, so the evaporation rate appears directly in the thickness law [3][2]. If heating doubles the evaporation rate and nothing else changes, the simple model predicts roughly double the capillary-regime thickness at the same speed.
That is the main reason for using a heated dip coater at low speeds. Temperature gives a second handle on the capillary branch besides speed, so a target thickness can sometimes be reached at a more convenient withdrawal speed. The same logic explains why capillary-regime results are sensitive to the room. A draught, a change in the vapour concentration above the bath or a warmer afternoon changes the evaporation rate and therefore the thickness. Heating can make the evaporation rate more repeatable if the surroundings are controlled, or less repeatable if the air around the meniscus is not.
Three cautions apply. First, the evaporation rate depends on airflow and vapour transport as well as temperature, so the effect of a given temperature change is specific to the set-up. Second, faster evaporation also changes how the solute deposits: in some systems a higher rate favours more uniform layers, while in others it promotes stick-slip deposition or stripes; this is system-dependent and must be checked. Third, in solutions near saturation, a warmer meniscus can change where and how quickly the solute crystallises, which affects film morphology as well as thickness.
5. Temperature in the draining regime
In the draining regime, the entrained wet thickness is set mainly by viscosity, speed and surface tension. Heating lowers viscosity for most liquids, so the wet film is usually thinner at the same speed [4][1]. Because the Landau–Levich exponent on viscosity is 2/3, the change in thickness is smaller than the change in viscosity.
Two complications matter in practice. First, evaporation does not stop in the draining regime. At moderate speeds the wet film loses solvent while it is still forming and draining, which increases its viscosity and solute content near the top of the meniscus. Heating strengthens this effect, so the dry thickness may fall less than the viscosity scaling alone suggests, or may even rise. Second, the dry thickness depends on the solute concentration in the bath, and a heated open bath loses solvent over time. Unless the bath is covered or topped up, the concentration drifts upward during a session, which thickens later films. A thickness series that drifts with time at a fixed speed and temperature is often a concentration effect.
6. How the thickness minimum moves
With the working form h ≈ A/U + B·U2/3, the minimum lies where the two contributions balance. Setting the derivative to zero gives the speed of the minimum, Umin = (3A/2B)3/5, and the minimum thickness scales as A2/5B3/5. These follow from the algebra of the model; they are not independent results.
Heating usually raises A, because evaporation is faster, and lowers B, because viscosity is lower. Both changes increase the ratio A/B, so both move the minimum to a higher speed. The effect on the minimum thickness itself depends on the balance between them.
The practical consequence is that a recipe written for room temperature can change branch when the bath is heated. A speed that gave a draining-regime film at room temperature may fall below the new minimum and enter the capillary branch, where slowing down makes the film thicker rather than thinner. If a temperature change produces an unexpected thickness trend with speed, check which side of the minimum each speed now sits on. The speed–thickness laws and fitting procedure are covered in The Landau-Levich Equation in Practice: Viscosity, Surface Tension and Speed.
7. Base, bath, substrate and meniscus temperature
A heated dip coater controls the temperature of a heating element, not directly the temperature at the point where the film forms. Between the two lie the container wall, the liquid, the substrate and the air above the bath. Each of these has its own temperature, and they settle at different rates.
- Base set-point. The value you enter. It is the temperature the controller aims to hold at its sensor.
- Bath temperature. Usually lower than a base set-point above ambient, because heat is lost from the liquid surface and the container walls. It also varies with depth, liquid volume and container material.
- Substrate temperature. A substrate immersed long enough approaches the bath temperature; a short immersion may leave a thick or poorly conducting substrate cooler than the liquid. Once withdrawn, the substrate cools in the air.
- Meniscus temperature. The surface of the meniscus loses heat by evaporation, so it can be cooler than the bulk bath. This is the temperature that matters most in the capillary regime, and it is the hardest to measure.
The practical rule is to report a measured bath temperature, not only the set-point, and to keep the immersion time, liquid volume and container the same across a series. A thermocouple or thermometer placed in the liquid near the substrate position, read after the bath has settled, gives a defensible number. If substrate temperature is important, immerse long enough for it to equilibrate, or measure it directly on a test piece.
Heating from below also sets up temperature differences within the bath, which can drive convection. Temperature differences along the meniscus can change the local surface tension and drive Marangoni flows. These effects are system-dependent; they are mentioned here as possible sources of non-uniformity, not as predicted outcomes.
8. Side effects of heating the solution
Heating changes more than thickness. Plan for the following side effects before starting a series:
- Solvent loss and concentration drift. An open, warm bath loses solvent continuously. Cover the bath between dips where the set-up allows, keep sessions short, and record the liquid level or mass so drift can be detected.
- Faster sol ageing. For reactive sols, hydrolysis and condensation usually speed up with temperature, so viscosity may rise during a session. The chemistry is described in Sol-Gel Dip Coating: From Sol to Dense Oxide Film (SiO2, TiO2) [8].
- Bubbles and boiling. Dissolved gas comes out of solution as the liquid warms, and bubbles on the substrate cause pinholes and streaks. Keep the bath well below the boiling point of the solvent. The base range of a heated dip coater may extend above the normal boiling points of common solvents such as ethanol (about 78 °C) and water (100 °C), so solvent hazards and equipment limits both constrain the working temperature.
- Vapour and flammability. A warmer bath releases more vapour. Work with ventilation suited to the solvent, keep ignition sources away and follow the safety data sheet, including the flash point and the autoignition temperature, since the heated base is itself a hot surface. Inside a glovebox, consider the solvent load on the atmosphere and its purification system.
- Condensation on cooler surfaces. Vapour from a warm bath can condense on cooler fixtures or on the substrate above the meniscus and drip back, leaving marks.
- Thermal stress and drying defects. Faster drying can increase stress in the drying film. Cracking and the critical thickness are treated by Brinker and Scherer [8] and in the sol-gel guide named above.
9. Planning a temperature–speed series
Because temperature changes both branches of the curve, a single coating at a new temperature tells you little. A small two-variable series gives a much clearer picture:
- Fix everything else. Use one solution batch, one container and liquid volume, one immersion time and one atmosphere. Record room temperature and humidity.
- Choose two or three temperatures. Start with room temperature as the reference and one or two higher bath temperatures well below the solvent boiling point.
- Let the bath settle. After each temperature change, wait until the measured bath temperature is stable before coating. Note the waiting time so it can be repeated.
- Run a full speed series at each temperature. Cover both low and moderate speeds, spaced roughly evenly on a logarithmic scale, so that both branches and the minimum appear.
- Randomise or interleave the speed order within each temperature where practical, so that slow drift in concentration or sol age does not masquerade as a temperature effect. Repeat the first condition at the end as a check.
- Measure thickness the same way every time, at the same position on each substrate, after the same drying step. Methods are compared in How to Measure Thin Film Thickness: Profilometry, Ellipsometry and Interference (coming soon).
- Fit each temperature separately. Where both branches are resolved, fit A and B and compare the contributions. The fit alone cannot distinguish changes in evaporation, viscosity and concentration.
| Observation when heated | Likely reading | Next check |
|---|---|---|
| Thicker at low speeds, little change at high speeds | Capillary branch raised by faster evaporation | Confirm with a second low-speed point; check airflow |
| Thinner at high speeds | Draining branch lowered by lower viscosity | Measure viscosity at the bath temperature if possible |
| Minimum appears at a higher speed | Ratio A/B increased, as expected | Re-select the working speed on the intended branch |
| All films thicker, worsening over the session | Solvent loss raising concentration | Cover the bath; repeat the first condition |
| Stripes or bands at low speed | Stick-slip deposition at the meniscus | Adjust speed, temperature or concentration; check substrate cleanliness |
| Pinholes after heating | Bubbles from dissolved gas or boiling near the surface | Lower the temperature; degas the solution |
Diagnostic guide only; each reading should be confirmed by measurement. The likely causes are general tendencies, not predictions for a specific solution.
10. What a heated dip coater page tells you
When comparing heated dip coaters, look for the motion range (especially the low end of the speed range for capillary-regime work), the heating range and what exactly is heated, the substrate size, programmable immersion and interval times, and whether the unit is designed for a glovebox. The table quotes the two single-bath Levon™ dip coater pages; “not stated” means a page does not give the value, not that the feature is absent.
| Specification | DP100-BE-H | DP100-BE |
|---|---|---|
| Heating | Heated base, RT to 120 °C, temperature controllable | Not stated |
| Running speed | 0.1–600 mm/min | 0.1–600 mm/min |
| Stroke | 0–100 mm (other strokes can be customized) | 0–100 mm (other strokes can be customized) |
| Immersion time | 1–9,999.9 s | 1–9,999.9 s |
| Repeat coating interval | 1–9,999.9 s | 1–9,999.9 s |
| Coating cycles | 1–999 | 1–999 |
| Max. substrate | ≤100 × 100 × 5 mm | ≤100 × 100 × 5 mm |
| Glovebox | Compact structure designed for placement in a glovebox | Compact structure designed for placement in a glovebox |
| Recipes | 100, named and stored | 100, named and stored |
Specifications as published on the Levon™ product pages on 22 October 2026. The DP100-BE-H page states a heated base with a range of RT to 120 °C; it does not state the bath, solution or substrate temperature reached, the heating rate, or the temperature uniformity. RT (room temperature) has no numeric value on the page and no cooling is stated. For glovebox use, check the antechamber size and internal height against the stated dimensions of 227 × 350 × 416 mm (W × D × H).
Read against the physics above, the lower end of the speed range, down to 0.1 mm/min, is where the capillary regime is likely to lie for many volatile solutions; a speed series shows where it begins for yours. The settable immersion time can be used to let a substrate approach the measured bath temperature before withdrawal. Because the page gives the base range rather than the liquid temperature, plan to measure the bath yourself. For a six-bath turntable instead of a single bath on a heated base, see the DP150-DR or the Levon™ dip coater category page.
11. Keep Exploring the Dip Coating Knowledge Hub
Start here
- Solution-Processed Thin Films: Choosing Spin, Dip, Slot-Die or Blade Coating — when dip coating is the right method, with the interactive coating method selector.
- Spin Coating Explained: Stages, Physics and Film Thickness — how evaporation and flow compete in the main alternative method.
Dip coating process guides
- Dip Coating Explained: Withdrawal Speed, Coating Regimes and Film Thickness — stages, regimes and the speed–thickness laws.
- The Landau-Levich Equation in Practice: Viscosity, Surface Tension and Speed — units, validity checks and fitting.
- Sol-Gel Dip Coating: From Sol to Dense Oxide Film (SiO2, TiO2) — sol chemistry, drying and heat treatment.
- Layer-by-Layer and Multi-Solution Dip Coating with a Carousel Dip Coater — sequential baths and rinses.
- How to Measure Thin Film Thickness: Profilometry, Ellipsometry and Interference (coming soon) — measuring each point of a series.
Links will be added as each article is published.
Levon™ dip coaters
- DP100-BE-H Heated Dip Coater — 0.1–600 mm/min with a heated base, RT to 120 °C, designed for placement in a glovebox.
- DP100-BE Dip Coater — the same motion range without a stated heating function.
- DP150-DR Carousel Dip Coater — six-position turntable for six standard 300 mL beakers, 240 mm maximum stroke.
- All Levon™ dip coaters — the dip coater category page.
Questions about a specific substrate, solution or configuration can be sent through the contact form.
12. FAQ
What does a heated dip coater do?
A heated dip coater adds temperature control to the usual withdrawal-speed control, typically through a heated element such as a base under the solution container. Heating changes the evaporation rate, viscosity and surface tension of the coating liquid, so temperature becomes a second variable for controlling film thickness and drying.
Does heating make dip-coated films thicker or thinner?
It depends on the regime. At very low speeds in the capillary regime, faster evaporation usually gives thicker films at the same speed. At higher speeds in the draining regime, lower viscosity usually gives thinner wet films. Running a speed series at each temperature shows which effect dominates for your solution.
Why does the thickness minimum move when I heat the bath?
The minimum sits where the capillary and draining contributions balance. Heating usually strengthens the evaporation-driven contribution and weakens the viscosity-driven one, so the balance point moves to a higher withdrawal speed. A speed that was on the draining branch at room temperature may then fall on the capillary branch.
Is the heated base temperature the same as the solution temperature?
Usually not. The bath loses heat through its surface and walls, the meniscus is cooled by evaporation, and the substrate may not reach the bath temperature during a short immersion. Measure the liquid temperature near the substrate after the bath has settled and report that value with the set-point.
How hot can I run a dip coating bath?
The solvent sets the practical limit, not only the instrument. Stay well below the boiling point to avoid bubbles and rapid solvent loss, and follow the safety data sheet for vapour and flammability. Reactive sols may also age faster when warm, so check viscosity or thickness drift during a session.