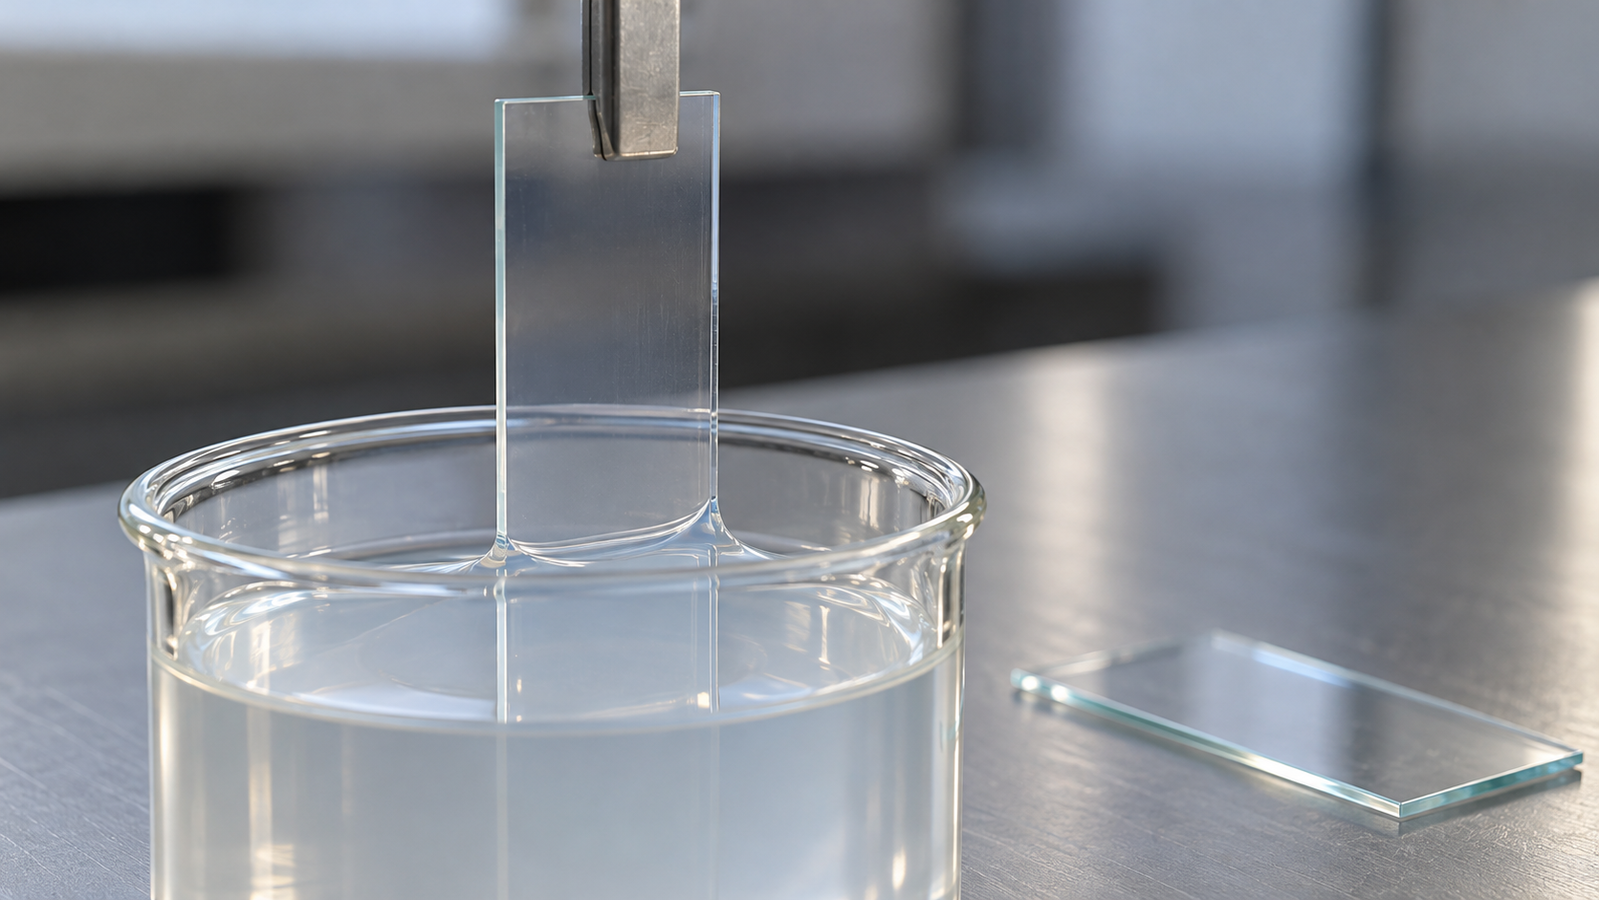
Sol-gel dip coating turns a liquid sol into a thin oxide film in three broad steps: a substrate is withdrawn from the sol at a controlled speed, the entrained layer gels and dries as solvent evaporates, and a heat treatment removes residual organics and densifies the film. This guide to sol-gel dip coating follows that path for the two most common oxides, silica (SiO2) and titania (TiO2). It explains the hydrolysis and condensation chemistry, what happens at the meniscus, why films crack, and how to plan a series of coatings you can reproduce.
In one paragraph: the sol chemistry decides what kind of network forms, and the dip coating step decides how much of it lands on the substrate. Silicon alkoxides react slowly and need a catalyst; titanium alkoxides react so quickly that they are usually moderated with acid or chelating ligands. Thickness follows the usual dip coating speed laws, then drying and firing shrink the film, and a film above a system-dependent critical thickness tends to crack. Build thicker films in several thin layers and measure thickness at each stage.
1. The short answer
Five points cover most practical decisions:
- The sol sets the network. Water content, catalyst, solvent and time decide whether the sol holds weakly branched species or denser clusters [1][2].
- Withdrawal sets the amount. Thickness rises with speed in the draining regime and with falling speed in the capillary regime [3][4].
- Gelation happens on the substrate, within a short drying zone above the bath [3].
- Drying and firing shrink the film, and a thick layer may crack.
- Build up in thin steps and measure the thickness after each stage.
If you are new to dip coating itself, the companion guide Dip Coating Explained: Withdrawal Speed, Coating Regimes and Film Thickness covers the stages and the speed–thickness laws in detail. For a comparison of dip coating with spin, slot-die and blade coating, see the pillar guide to solution-processed thin films.
2. Sol-gel chemistry: hydrolysis and condensation
Most oxide sols for dip coating start from metal alkoxides, M(OR)n, where M is a metal or silicon and OR is an alkoxy group such as ethoxy or isopropoxy. Two families of reactions convert the dissolved precursor into an oxide network [1][2]. Written for silicon, they are:
Water condensation: ≡Si–OH + HO–Si≡ → ≡Si–O–Si≡ + H2O
Alcohol condensation: ≡Si–OR + HO–Si≡ → ≡Si–O–Si≡ + ROH
≡Si represents a silicon atom bonded to three further groups; R is an alkyl group
Hydrolysis replaces alkoxy groups with hydroxyl groups. Condensation links two hydroxylated (or partly hydrolysed) centres through an oxygen bridge and releases water or alcohol. The reactions run in parallel and are usually reversible to some degree, so a sol is a changing mixture of species, not a fixed compound.
Several variables steer the balance between hydrolysis and condensation, and with it the shape of the growing species [1]:
- Water ratio. The molar ratio of water to alkoxide (often written r or R) controls how completely the precursor can hydrolyse. Low ratios leave unhydrolysed alkoxy groups that limit branching; higher ratios allow more complete hydrolysis.
- Catalyst and pH. For silica, acid catalysis tends to favour weakly branched, polymer-like species, while base catalysis tends to favour more highly branched clusters or particles. This is the main reason acid-catalysed silica sols are often chosen for dense films and base-catalysed sols for porous or particulate films [3].
- Solvent. An alcohol solvent makes water and alkoxide miscible and sets the evaporation rate during coating. Because alcohol is also a reaction product, its amount influences the reverse reactions.
- Time and temperature. Condensation continues while the sol is stored, so its viscosity and the size of its species change with age.
These are tendencies, not rules with fixed thresholds, so record a sol’s full preparation history.
3. Silica and titania sols compared
Silica and titania are the two oxides most often used to learn sol-gel dip coating, and their chemistry differs in ways that matter at the bench. Silicon alkoxides hydrolyse relatively slowly and need a catalyst. Transition metal alkoxides such as titanium alkoxides are far more reactive, because the metal is less electronegative and can increase its coordination number. Uncontrolled addition of water can therefore precipitate titanium oxo-hydroxide particles instead of forming a coatable sol [5]. Their reactivity is commonly moderated in two ways [5]. Complexing ligands, such as acetylacetone or acetate from acetic acid, replace some alkoxy groups and make the precursor less reactive toward water. Strong acids, such as hydrochloric or nitric acid, act differently: they keep the hydrolysed species positively charged, which slows condensation and keeps small particles dispersed (peptisation).
| Aspect | Silica (SiO2) sols | Titania (TiO2) sols |
|---|---|---|
| Typical precursor family | Silicon alkoxides, e.g. tetraethyl orthosilicate (TEOS) | Titanium alkoxides, e.g. titanium isopropoxide or butoxide |
| Reactivity with water | Slow; acid or base catalyst normally used | Fast; can precipitate if water is added without control |
| Common moderation | Choice of catalyst, water ratio and dilution | Acid, chelating ligands, low water content and dilution |
| Handling | Moisture in air matters for sol stability and film formation | More sensitive to humidity; dry atmosphere often preferred during preparation |
| Structure after drying | Amorphous silica network, dense or porous depending on the sol | Usually amorphous; crystallizes on heating |
| Optical role | Low refractive index; porosity lowers it further | High refractive index |
| Typical uses of films | Barrier layers, antireflection and porous layers, matrices for hybrids | High-index optical layers, photocatalytic and electronic layers |
General tendencies from the sol-gel literature [1][2][5]. Specific reactivity, stability and film structure depend on the precursor, additives, solvent and process conditions.
The contrast in refractive index is why silica and titania are often combined in optical multilayers: alternating low- and high-index layers can be built by dipping into two sols in turn, with a drying or heat-treatment step between layers. Multi-solution sequences are covered in Layer-by-Layer and Multi-Solution Dip Coating with a Carousel Dip Coater.
4. Preparing a sol for dip coating
A sol that is chemically correct can still coat poorly. For dip coating, five properties of the liquid matter as much as its composition:
- Solid content. The oxide-equivalent concentration sets both the viscosity and the fraction of the wet film that remains after drying. It is often the simplest lever for thickness at a fixed speed.
- Viscosity. In the draining regime the wet thickness scales with viscosity to the power 2/3 [6][3]. Viscosity rises as condensation proceeds, so it should be checked when the sol is used, not only when it is made.
- Stability and aging. A sol that is still growing changes from day to day, and close to its gel point it may not coat at all. Many workflows define an aging step and a usable window, and note the sol age with each coating.
- Cleanliness. Dust, gel fragments and precipitated particles cause comets, pinholes and haze. Filtering the sol before use and keeping the bath covered between runs reduce them.
- Wetting. The sol must wet the substrate completely. Substrate cleaning, and sometimes surface activation, come before any coating.
Because hydrolysis consumes water, humidity above the bath affects both the sol and the film. Covered baths, enclosures and dry atmospheres make the environment repeatable; especially moisture-sensitive precursors are sometimes handled in a glovebox.
5. At the meniscus: from sol to gel film
Dip coating is usually described in stages: immersion, start-up, deposition, drainage and evaporation [7]. In sol-gel dip coating with volatile alcohol solvents, drainage, evaporation and gelation overlap. Brinker and co-workers described a wedge-shaped drying zone above the bath in which the entrained sol thins by drainage and evaporation at the same time [3]. Within this zone:
- The sol concentrates. Solvent evaporates from the thin layer, so the inorganic species are packed more closely.
- Species aggregate and gel. As the concentration rises, condensation and aggregation link the species into a network that spans the film. The film can no longer flow.
- The gel compacts. Further evaporation removes liquid from the pores. Capillary pressure collapses the network until it is stiff enough to resist further shrinkage.
Brinker and co-workers noted that the short time scale and the shear and compaction during drying make dip-coated gel films structurally different from bulk gels made from the same sol [3][8]. Weakly branched species can interpenetrate and pack densely before they gel, while compact clusters tend to leave more pore space. This is one reason the sol chemistry in Section 2 carries through to the porosity of the final film.
Wet-film entrainment and evaporative deposition follow different thickness scalings [4][9]:
Draining regime, dried film (no lateral shrinkage): hdry ≈ φ · hwet ∝ U2/3
Capillary regime (fixed sol and evaporation conditions): hdry ∝ U−1
η = viscosity; U = withdrawal speed; γ = surface tension; ρ = density; g = gravitational acceleration
The Landau–Levich expression [6] gives the entrained wet layer for a Newtonian liquid at low capillary number. For sols it is a guide to scaling rather than an exact prediction, because evaporation and gelation start while the layer is still forming. In the capillary regime, solute deposits directly at the meniscus as the solvent evaporates, and the deposited thickness increases as speed falls [4]. The equation itself is worked through in The Landau-Levich Equation in Practice: Viscosity, Surface Tension and Speed. Temperature shifts evaporation and the position of the capillary regime, which is the subject of Heated Dip Coating: How Temperature Shifts Evaporation and the Capillary Regime.
6. Drying, shrinkage and cracking
As solvent leaves the pores of a gel film, curved liquid menisci in the pores pull on the network. For a cylindrical pore, the Young–Laplace equation gives the order of magnitude of this capillary pressure [1]:
γ = liquid–vapour surface tension; θ = contact angle of the liquid on the pore wall; rp = pore radius
The smaller the pores, the larger the pressure, so fine-pored gels experience large stresses as they dry. A free bulk gel can shrink in all directions. A film bonded to a rigid substrate can shrink only through its thickness, so in-plane tensile stress builds up. If the stored elastic energy exceeds what is needed to open a crack, the film cracks [1].
A practical consequence, widely reported for sol-gel films, is a critical thickness: below it, films tend to dry without cracking; above it, cracks become likely. It is not a universal number; it depends on the sol, drying rate, substrate and heat treatment, and has to be found experimentally. Common remedies:
- Coating thinner layers, by lowering the solid content or choosing a speed that gives a thinner film.
- Drying more slowly and uniformly, for example under a cover or in a solvent-rich atmosphere.
- Changing the sol chemistry, for example its catalyst, water ratio, or organic modification of the network.
- Building thickness in several layers, each dried or heat-treated before the next (Section 8).
Drying shrinkage is also the reason why a wet-film estimate overstates the final thickness. A first estimate of the dried thickness is the wet thickness multiplied by the volume fraction of non-volatile material. Residual porosity makes the real film thicker than this estimate, and later densification makes it thinner [1][8].
7. Heat treatment: from gel to oxide
A dried gel film still contains water, residual alkoxy and hydroxyl groups, and any organic additives. Heat treatment converts it into an oxide film through overlapping processes [1][8]:
- Removal of physically held solvent and water from the pores.
- Further condensation of remaining hydroxyl and alkoxy groups, which releases more water and alcohol and stiffens the network.
- Removal of organics such as residual alkoxy groups, chelating ligands and templating agents, usually by oxidation in air.
- Densification, in which pores shrink or close and the film becomes thinner.
- Crystallization for oxides such as titania. Titania films are typically amorphous after drying and crystallize on heating. Anatase is commonly the first crystalline phase in sol-gel titania; the temperature at which it forms depends on the precursor, additives, film thickness, substrate and heating schedule.
Silica films remain amorphous under ordinary processing; heat treatment mainly removes residues and densifies them. The rate of heating matters as well as the final temperature. Rapid heating can trap organics or produce gas faster than it can escape, and stresses from densification and thermal expansion mismatch add to those from drying. The substrate sets an upper limit: the temperature it tolerates may be well below what full densification or a target crystal phase would require.
This guide gives no heat-treatment temperatures, because suitable values differ between precursors, substrates and target structures. Start from published procedures for your system and confirm with your own measurements. A thermogravimetric run on dried gel from the same sol shows roughly where solvent and organics leave, and X-ray diffraction after trial firings shows when a crystalline phase appears; films can behave differently from powders, so record the heating rate and dwell with each film.
8. Building thickness with several layers
When a film thicker than the crack-free limit is needed, or a stack of different oxides, the coating is repeated. A typical multilayer cycle is: dip and withdraw; dry; optionally heat-treat; cool; repeat. Three points determine whether this works:
- Redissolution. A freshly gelled layer that has not been dried or heat-treated may partly redissolve or swell when it is dipped again. Intermediate drying or heat treatment stabilizes each layer.
- Wetting of the new surface. The second and later dips deposit onto the previous film, not onto the bare substrate. If the surface energy has changed, wetting and entrained thickness can change too.
- Accumulated stress. Stress builds up with each layer, so a stack can crack even when each single layer does not. Inspecting the film after each few layers shows where the limit lies.
The thickness per cycle is therefore not guaranteed to be constant; measure the total rather than multiplying a single-layer value. Programmable cycles, immersion and interval times suit multilayers dried on the instrument, while heat treatment between layers is usually done separately, for example on a hotplate or in a furnace.
9. Planning a sol-gel coating series
A short, well-documented series gives more usable information than many unrelated runs. One practical sequence:
- Fix the sol. Use one batch, record its preparation (precursor, solvent, water ratio, catalyst, additives) and its age at each coating.
- Fix the environment. Record temperature and humidity at the bath, and keep the bath covered or enclosed in the same way for every run.
- Run a withdrawal-speed series with speeds spread on a logarithmic scale, so that both draining and, if present, capillary behaviour can appear.
- Measure the thickness at each stage: after drying and again after heat treatment, in the same central region of each film. A dedicated article, How to Measure Thin Film Thickness: Profilometry, Ellipsometry and Interference (coming soon), will cover these methods.
- Inspect for cracks and haze at each stage, so that the crack-free limit is found alongside the thickness curve.
- Change one thing at a time afterwards: solid content, sol age or heat-treatment schedule.
Illustrative bookkeeping. Suppose a dried single layer measures 200 nm, and a firing step reduces its thickness by an assumed 40%. The fired layer is then 200 nm × (1 − 0.40) = 120 nm. A target of about 360 nm would suggest three layers, if every layer behaved identically, and that assumption is exactly what the series must test.
The 200 nm thickness and the 40% reduction are assumed values chosen to illustrate the calculation. They are not results from any sol, dip coater or Levon™ instrument.
10. Common defects and their causes
| Defect | Likely causes | What to try |
|---|---|---|
| Cracks or crazing | Layer above the critical thickness; fast drying; stress from heat treatment | Thinner layers; slower, covered drying; several layers; gentler heating |
| Haze or cloudiness | Particles or precipitate in the sol; uncontrolled hydrolysis; high humidity | Filter the sol; check its age; control humidity; moderate the precursor |
| Comets and pinholes | Dust, gel fragments or bubbles | Filtered sol; clean substrate and bath; covered bath between runs |
| Dewetting or bare patches | Incomplete wetting of the substrate | Improve cleaning; check the solvent; consider surface activation |
| Horizontal bands | Speed fluctuation or vibration during withdrawal; draughts | Rigid stand; shield the bath; keep the withdrawal speed constant |
| Thickness gradient along the substrate | Drainage before gelation; changing evaporation along the stroke | Faster-drying solvent (less drainage before gelation) or an enclosure (more uniform evaporation); check the regime; discard the start-up zone |
| Thick bottom edge | Liquid bead collecting where the substrate leaves the bath | Touch the bottom edge to lint-free absorbent paper to wick off the bead, or treat the bottom few millimetres as sacrificial; validate any change in final withdrawal speed |
Typical associations from sol-gel and dip coating practice; several causes can act together, so change one variable at a time when diagnosing.
11. Dip coater features for sol-gel work
For sol-gel films, the instrument features that matter most are the speed range (for mapping coating regimes and the thickness minimum), stroke and substrate size, programmable immersion time, interval and cycles (for multilayers with an on-instrument drying step), placement in a controlled atmosphere, and heating. The table quotes the three Levon™ dip coater pages; “not stated” means a page does not give the value, not that the feature is absent.
| Specification | DP100-BE | DP100-BE-H | DP150-DR |
|---|---|---|---|
| Running speed | 0.1–600 mm/min | 0.1–600 mm/min | 0.1–600 mm/min |
| Stroke | 0–100 mm (other strokes can be customized) | 0–100 mm (other strokes can be customized) | Max. 240 mm |
| Immersion time | 1–9,999.9 s | 1–9,999.9 s | 0–9,999.9 s |
| Repeat coating interval | 1–9,999.9 s | 1–9,999.9 s | 0–9,999.9 s |
| Coating cycles | 1–999 | 1–999 | 1–999 |
| Max. substrate | ≤100 × 100 × 5 mm | ≤100 × 100 × 5 mm | ≤150 × 150 × 5 mm |
| Heating | Not stated | Heated base, RT to 120 °C, temperature controllable | Not stated |
| Glovebox | Compact structure designed for placement in a glovebox | Compact structure designed for placement in a glovebox | Not stated |
| Displacement accuracy | ±0.01 mm | ±0.01 mm | ±0.1 mm |
| Solution positions | Not stated | Not stated | Six-position turntable, six standard 300 mL beakers |
| Recipes | 100, named and stored | 100, named and stored | 100, named, stored and recalled |
Specifications as published on the Levon™ product pages on 22 October 2026. The DP100-BE-H page states a heated base; it does not state the bath, sol or substrate temperature reached. RT (room temperature) has no numeric value on the page and no cooling is stated. None of the pages describes oxide heat treatment, which is normally done separately. For glovebox use, check the antechamber size and internal height against the stated dimensions of 227 × 350 × 416 mm (W × D × H).
For moisture-sensitive single sols, the two DP100 models are designed for placement in a glovebox; for stacks of two or more sols, the DP150-DR carries six beakers on a turntable. See the Levon™ dip coater category page.
12. Keep exploring the dip coating knowledge hub
Start here
- Solution-Processed Thin Films: Choosing Spin, Dip, Slot-Die or Blade Coating — when dip coating is the right method, with the interactive coating method selector.
- Spin Coating Explained: Stages, Physics and Film Thickness — the main alternative for one-sided sol-gel films on flat substrates.
Dip coating process guides
- Dip Coating Explained: Withdrawal Speed, Coating Regimes and Film Thickness — stages, regimes and the speed–thickness laws.
- The Landau-Levich Equation in Practice: Viscosity, Surface Tension and Speed — units, validity checks and worked examples.
- Layer-by-Layer and Multi-Solution Dip Coating with a Carousel Dip Coater — sequential baths, rinses and oxide stacks.
- Heated Dip Coating: How Temperature Shifts Evaporation and the Capillary Regime — temperature, evaporation and the thickness minimum.
- How to Measure Thin Film Thickness: Profilometry, Ellipsometry and Interference (coming soon) — measuring dried and fired films.
Links will be added as each article is published.
Levon™ dip coaters
- DP100-BE Dip Coater — 0.1–600 mm/min, 0–100 mm stroke, substrates to 100 × 100 mm, designed for placement in a glovebox.
- DP100-BE-H Heated Dip Coater — the same motion range with a heated base, RT to 120 °C.
- DP150-DR Carousel Dip Coater — six-position turntable for six standard 300 mL beakers, 240 mm maximum stroke, substrates to 150 × 150 mm (the bath container may set a smaller practical limit).
- All Levon™ dip coaters — the dip coater category page.
Questions about a specific substrate, sol or configuration can be sent through the contact form.
13. FAQ
What is sol-gel dip coating?
Sol-gel dip coating is a way of making oxide films by withdrawing a substrate from a sol, usually prepared from metal alkoxides, at a controlled speed. The entrained layer gels as the solvent evaporates, and drying and heat treatment convert the gel into a dense or porous oxide film such as silica or titania.
Why do titania sols need more control than silica sols?
Titanium alkoxides react with water much faster than silicon alkoxides, so uncontrolled hydrolysis can precipitate particles instead of forming a coatable sol. Chelating ligands such as acetylacetone are commonly added to slow hydrolysis, acids to slow condensation and keep particles dispersed, and a dry atmosphere is often preferred during preparation.
Why does my sol-gel film crack?
Cracks usually form when drying or heat-treatment stresses in a substrate-bonded film exceed what the network can withstand. Films above a system-dependent critical thickness are most at risk. Thinner layers, slower drying, adjusted sol chemistry and building thickness in several layers are the usual remedies.
Does withdrawal speed matter in sol-gel dip coating?
Yes. In the draining regime the entrained thickness increases with speed, roughly as speed to the power 2/3. At very low speeds with volatile solvents the capillary regime applies, and slower withdrawal gives thicker films. A speed series with measured thickness shows which applies to your sol.
At what temperature should I fire a sol-gel film?
There is no single answer. The temperature needed to remove organics, densify the film or reach a crystal phase depends on the precursor, additives, film thickness, substrate and heating rate, and the substrate may set an upper limit. Start from published procedures for your system and confirm with thickness and structure measurements.