Lab-scale polymer processing uses small quantities of material to study how preparation, mixing and shaping affect a polymer and its test results. This guide organizes that work into five stages, material, compound, shape, specimen and test, which may be combined or omitted depending on the starting material and measurement. It explains what each stage decides and places every machine of the Polytevo Series by ACS Material in the stage where it is used, using only what the product pages say.
1. The short answer: five planning stages
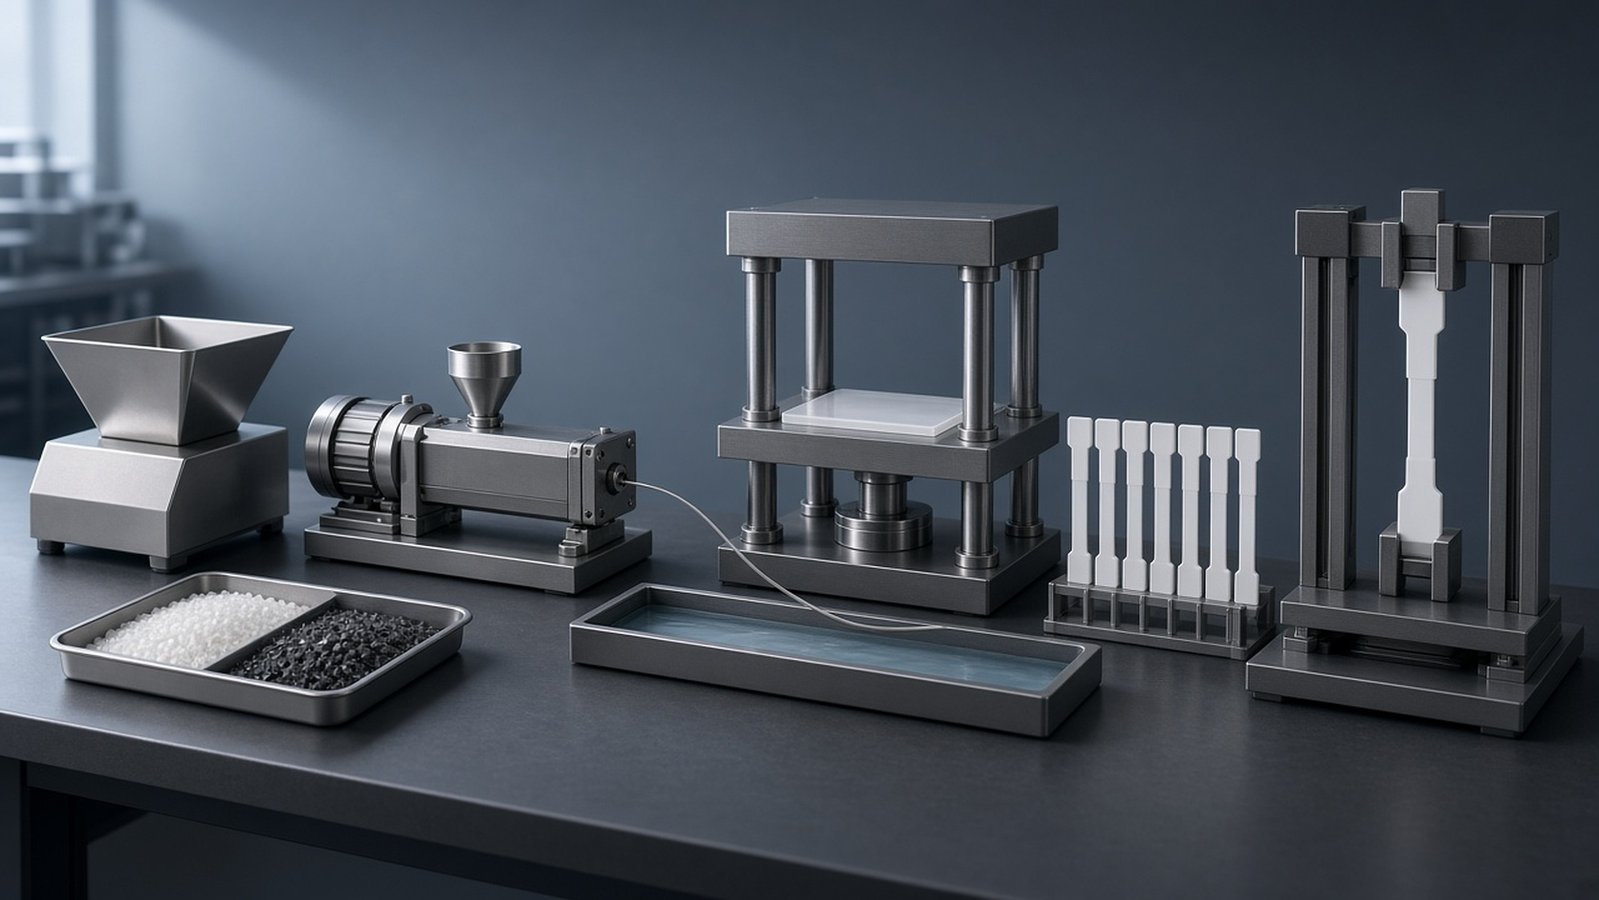
The short answer to “how do I set up lab-scale polymer processing and testing?” is to plan the work as a route rather than as a list of machines. This guide organizes the work into five planning stages: material, compound, shape, specimen and test. They are not mandatory separate operations. Depending on the starting material and the measurement, stages may be combined, repeated or omitted.
- Material. Decide exactly what goes into the machine: its form, its size, its moisture and its history.
- Compound. Turn a mixture of resin, filler and additive into a uniform melt, strand or pellet.
- Shape. Turn the melt into the form the test needs: a strand, a film, a filament, a pipe, a plate or a molded part.
- Specimen. Turn that shape into a test piece of defined geometry, free of damage, with a notch if the method calls for one.
- Test. Choose the property first and the instrument second, then run it under conditions that are written down.
Each stage that is carried out hands something to the next one and leaves a record behind it. A test result that arrives without those records is a number; with them it is evidence that someone else can repeat or challenge. That is the whole idea of this guide.
What “lab-scale” means here
In this guide lab-scale means grams to a few kilograms of material on a bench machine, used to learn how a material behaves rather than to produce goods. That range is a working judgment, not a standard, and the machines in the route differ a good deal in how much material they need before they run steadily.
What a lab-scale result describes is the material on that machine under those conditions. Scale-up of mixing and melting has been studied for specific machine types, and section 4 returns to this. A bench result is therefore evidence about the material and a good reason to ask the production question; it is not a prediction of the production answer.
How to read this guide
Sections 3 to 7 take the stages one at a time. In each of them the general science comes first, with its sources, and the product statements follow in their own paragraphs, so that you can always tell what is general polymer science and what a Polytevo product page says. Section 8 holds the one table that places every Polytevo Series page, all 31 of them, in the stage where it is used. Sections 9 and 10 show two illustrative routes and the record to keep at each stage.
Product statements in this guide are what the product pages said on 15 November 2026. They give names and roles only, never specifications, so that this guide does not go stale when a page is updated; the pages remain the place to read specifications, and final configurations are confirmed on quotation.
2. The route at a glance
The table sets the five stages side by side. Read it from left to right for one stage, and from top to bottom for the path a sample takes.
| Stage | The question it answers | What it hands to the next stage | The record to keep |
|---|---|---|---|
| Material | What exactly is going into the machine? | Material of known form, size and moisture | Resin identity and lot, form, size reduction done, drying state |
| Compound | Is the mixture uniform, and what did the melt go through? | A strand, pellets or melt of known composition | Formulation by mass, machine and set-up, temperatures, speeds, time in the machine |
| Shape | Which form does the test need, and what did forming do to the material? | A strand, film, filament, pipe, plate or molded part | Forming route, melt and tool temperatures, pressure, time, cooling, flow direction |
| Specimen | Is the test piece the right shape, undamaged and repeatable? | Specimens of defined geometry | Preparation method and tool, notch if any, number prepared, conditioning |
| Test | Which property, under which conditions, with what spread? | A result together with its conditions | Instrument, method reference, conditions, number of specimens, how the result is reported |
Two features of the route are worth seeing before the details. First, the work required at each stage depends on the starting material and the intended measurement. Whatever the effort, a test can only measure the specimen it is given, so the records of the earlier stages matter even when those stages were short. Second, the stages are separable. A laboratory that buys its compound can start at stage three; one that only tests can start at stage five, provided the records of the earlier stages travel with the specimens.
Each stage has a body of practice of its own, and this guide gives each only as much room as the route needs. Later guides in this library go deeper: choosing a laboratory extruder, matching a mechanical or hardness test to the question, reading the melt flow and heat lines of a datasheet, molding test specimens, preparing specimens, extrusion lines and output forms, compounding and material preparation, and dispersion and quality control. Section 11 lists them.
3. Stage 1, material: know what goes in
Every later stage inherits what the first one leaves unsaid. A resin lot, a regrind batch and a masterbatch are different starting points even when they carry the same polymer name, and the cheapest way to avoid an argument about a result is to describe the starting point before the first machine is switched on.
Form and history
Polymer arrives at the bench as pellets, powder, regrind or scrap film, and the form matters before any heat is applied. A screw extruder starts by conveying solid material forward, then melts it, then pumps the melt;1,2 how freely a feed runs from the hopper into the screw depends on its size, shape and fines, so the same polymer as pellets and as powder can behave quite differently at the feed throat. Powders and regrind can also carry more moisture and trapped air than pellets, and moisture-sensitive resins need a defined dry state before melt processing. The drying conditions come from the resin datasheet and the method reference, and the state the material was actually in belongs in the record.
History matters as much as form. Material that has been molded, ground and reprocessed has been heated and sheared before, and mixed scrap can contain more than one polymer. A review of mechanical recycling lists related challenges: sorting, thermo-mechanical or lifetime degradation, and the immiscibility of polymer blends.3 For a laboratory the practical rule is simple: never mix lots silently, and write down what the material has been through, because a regrind specimen and a virgin specimen can differ from the first stage onward.
Size reduction and pre-blending
Two machines belong to this stage, one that reduces size and one that mixes before the melt.
Size reduction produces a regrind whose particle size depends on the screen and the material, which in turn affects how the regrind feeds in the next stage. The screen used is one more line for the material record.
The Polytevo Series Laboratory Plastic Shredder page describes crushing hard-plastic sprue and runner scrap from injection molding in small laboratory batches, with a selectable screen mesh and a frequency converter fitted, and it describes the machine as suited to recovering small batches and expensive materials in the laboratory.
Pre-blending establishes the feed composition and distribution. It does not by itself demonstrate the dispersion obtained after subsequent processing; assess that dispersion separately. Writing the pre-blend into the record, with its composition by mass, keeps pre-blending and dispersion from being confused later.
The Polytevo Series High Speed Mixer page describes mixing and coloring PVC resin, coloring and drying PE and PP pellets, and mixing hygroscopic resins such as ABS and polycarbonate before molding and processing. It also describes friction heat generated during high-speed movement, with heating or cooling added as required.
The material record
The material record is short, and it is the first of the five records in section 10. At a minimum it names the resin and the lot, the form, any size reduction and the screen used, the drying state, the additive or filler and its lot, and the composition by mass. If the sample is regrind, it adds where the scrap came from. Record these details during preparation; reconstructing them later may be unreliable.
4. Stage 2, compound: from mixture to melt
Compounding turns a loose mixture into a uniform melt. Two things happen in it: the polymer melts, and the additive or filler is mixed into it. The first involves heat transfer and mechanical energy dissipation; the second is where machines differ most, and it affects every later specimen.
Single-screw, twin-screw, conical and recirculating machines as a decision
A single-screw extruder is above all a melting and pumping machine: solids are conveyed forward, melted by heat from the barrel and by the work done on the material, and the melt is pumped to the die.1,2 Melting is not only conduction from the barrel wall. Studies of melting in internal mixers and in co-rotating twin-screw extruders show that heat generated by deforming and rubbing solid particles contributes substantially,4 which is why a setpoint on the controller is not the temperature the melt actually reaches, and why a melt temperature reading, when the machine has one, is worth recording.
Mixing comes in two kinds. Distributive mixing spreads components evenly without breaking them; dispersive mixing breaks agglomerates and droplets apart.5 A plain single screw does a modest amount of both unless it carries mixing sections. Intermeshing twin-screw machines, whose screws are built up from conveying and mixing elements, are often chosen when stronger and more adjustable mixing is needed, and co-rotating designs are described in detail in the literature on twin-screw compounding.6 That is the main reason a laboratory chooses between machine types: not output, but how hard and how adjustably the machine works the mixture.
The Polytevo pages describe a small family of machines for this stage, and it helps to read them as answers to different questions:
- Straight melt processing. The Polytevo Series Single Screw Extruder page describes mixing and processing of engineering plastics, modified plastics, masterbatch and other polymers, with a cooling tank and an air-drying and pelletizing unit supplied. The Polytevo Series Benchtop Single-Screw Extruder page describes a benchtop micro machine for teaching demonstrations and small-batch extrusion.
- Compounding with a specimen at the end. The Polytevo Series Benchtop Mini Extruder page describes a compact benchtop system for compounding new materials and producing small-batch extruded specimens, with a mold clamping mechanism built in.
- Circulating the batch. The Polytevo Series Recirculating Single-Screw Extruder page describes a circulating flow channel and a reversing valve, so that material can be circulated through the screw and barrel for mixing or switched to extrusion.
- Micro-sample blending. The Polytevo Series Conical Twin-Screw Extruder page describes micro-sample blending of new or costly materials, with quick-release screws, a fully opening chamber and rheology control software with several blending modes. The Polytevo Series Dual Conical Twin-Screw Extruder page describes conical twin-screw sets with independently adjustable speeds for micro-sample blending and modification experiments with highly filled and high-viscosity materials.
- Twin-screw compounding and pelletizing. The Polytevo Series Twin-Screw Extrusion and Pelletizing Line page describes a co-rotating twin-screw compounding line for PE and PP formulations with vacuum venting and a strand pelletizing system.
Roll mixing versus melt mixing
A two-roll mill works the material in the gap between two heated rolls and hands it back as a sheet. Open rolls make the material visible, but sampling and cut-and-fold work require the machine’s specified safeguarding and an approved operating procedure. Operator actions remain part of the method for both open and closed systems, so the number of passes, the gap and the time on the rolls have to be written down as carefully as a screw speed would be.
The Polytevo Series Two-Roll Mill page describes thermal plasticating, mixing and dispersion of polymers in laboratory and small-batch work, with electric heating, dual servo motors and a roll gap set by handwheel.
Small batch versus continuous
The second decision is how the machine uses material. Batch or recirculating operation processes a defined charge for a selected period. Continuous operation feeds and discharges material during the run, but filling alone does not establish stable operating conditions; define and record the startup and sampling criteria used for a comparison.2 The product pages publish batch-size or output figures for several of these machines; the practical test is to compare those figures with the quantity of precious material you actually have, before choosing.
Torque recorded during compounding is additional process information about how the melt behaved, and it belongs in the compound record alongside the set conditions.
The Polytevo Series Conical Twin-Screw Extruder page describes torque measurement, and its rheology control software supports single-cycle, timed-cycle, continuous feeding, constant-speed and constant-torque blending.
What lab scale does and does not tell you about production
Small machines have a high ratio of wall area to melt volume, so they gain and lose heat differently from production machines, and their screws and chambers have different geometry from the machines that will run the same formulation later.2 Scale-up has been studied for specific systems. Bigio and Wang investigated distributive-mixing scale-up in partially filled, non-intermeshing counter-rotating twin-screw extruders at two sizes.7 Their findings are specific to that system and do not provide a general transfer rule for the other machines in this guide. The honest use of a lab compounding result is therefore comparative: this filler, run through this route, gave a better or worse specimen than the control run through the same route. Such a comparison is informative when preparation, test conditions and variability are documented. A claim that the same formulation will behave identically at production scale is not something a bench result can carry on its own.
The record for this stage is the second of the five: formulation by mass, the machine and its set-up, the temperature profile and the melt temperature if read, speed, feed rate, time in the machine or number of cycles, and for a mill the gap and the passes.
5. Stage 3, shape: extrudate, film, filament, part
Shaping gives the melt the form the test will need. It is also the stage where the material acquires much of its test-relevant history: the molecular and filler orientation set by flow, the cooling rate, the residual stress, the voids. Two specimens of the same compound shaped by different routes are specimens with different processing histories and potentially different measured properties.
Extrusion lines and what comes out
An extrusion line is an extruder followed by a die and by the equipment that draws and cools what comes out. The shape is fixed after the die, by the drawing, the cooling and the sizing, which is why the downstream equipment matters as well as the screw. The Polytevo pages describe five lines, each for a different output:
- Pipe. The Polytevo Series Single-Screw Pipe Extrusion Line page describes small-batch production of small-diameter pipes, with a vacuum sizing tank, a caterpillar haul-off and a fly-knife cutter.
- Filament. The Polytevo Series 3D Printing Filament Extrusion Line page describes laser diameter measurement that feeds back to the traction assembly in a closed loop, with automatic winding onto standard spools.
- Fiber-core filament. The Polytevo Series Fiber-Core 3D Printing Filament Coating Line page describes coating continuous fiber cores, such as carbon fiber and glass fiber, with thermoplastic material to make reinforced filament, with in-line diameter measurement.
- Cast film. The Polytevo Series Cast Film Extrusion Line page describes cast film forming experiments with polymer materials, performance testing of new materials for casting, and dispersion performance testing of color masterbatches.
- Blown film. The Polytevo Series Film Blowing Machine page describes double-fold blown film from a continuously extruded melt expanded by compressed air, cooled by a cooling ring and drawn by variable-frequency traction, used to evaluate film-blowing feasibility and to assess melt gel content and dispersibility.
For filament, the literature describes the surrounding problem. A review of fused deposition modeling starts from filament production and maps how the filament, the material and the printing parameters together affect the printed result.8 Yu et al. studied diameter control for filaments deposited during extrusion 3D printing, a different operation from producing spool-fed printing filament.9 Diameter, and its variation along the length, are worth recording in the shape record. What happens to the filament afterwards is compared in FDM vs SLA vs SLS: Polymer 3D Printing Processes Compared.
Tian et al. studied the relationship between processing, interface formation and performance in printed continuous-carbon-fiber/PLA composites.10 This research does not establish the performance of a separate fiber-coating line, so the coating and printing conditions go in the record with the filament.
The film bubble is a flow problem of its own; its mathematics goes back to the treatment of the flow of a thin tubular liquid film,11 and the practice is covered at book length.12
Film is worth a moment because it does double duty. A film is a test shape for film properties, and it is also a magnifying glass for the compound: undispersed particles and gels that are invisible in a pellet show up in a thin film. Both film pages say so for their own uses, and the record should say which of the two jobs the film was made to do.
Injection and transfer molding
Molding gives a part of defined geometry, which is why it is often the route to test bars.
The Polytevo Series Precision Injection Molding Machine page describes compact precision injection molding machines, a pneumatic one (ACS-7003) and a hydraulic one (ACS-7003H), with specimen types that include stretch, impact, light transmittance, electric breakdown, shrinkage, fluidity, thermal deformation and color plate, and with a fast-changing mold core and an optional specimen mold.
The Polytevo Series Vertical Transfer Molding Machine page describes a different principle: compounded material is softened in a heated barrel, pressed by a pneumatic piston through a runner into a preheated mold, and held and cooled before the specimen is removed. It names dog-bone tensile, flexural, impact and color plaque specimens.
For injection-molded test specimens, the cited molding practice notes that preparation conditions can affect measured properties.13 In a study of short-glass-fiber-reinforced PBT, filling time, melt temperature, mold temperature and packing pressure changed the tensile properties, because they changed how the fibers were oriented in the part.14 Test method reference: ISO 294-1:2017 and ASTM D3641-24 for molding specimens from thermoplastics.13,15 Record the barrel and mold temperatures, injection and holding conditions, and cooling time. Choose preparation conditions appropriate to each material and the applicable method. Hold the intended comparison variables constant where appropriate, and report any necessary differences in preparation conditions.13,15
Plate pressing
Pressing makes a flat plaque from which specimens are cut. Compression molding imposes a different flow history from injection molding; specimen preparation and cooling still need to be controlled for a meaningful comparison.
Test method reference: ISO 293:2023 addresses compression molding of test specimens from thermoplastics but excludes reinforced thermoplastics.16 For a reinforced formulation, select a preparation procedure that applies to that material.
The Polytevo Series Plate Vulcanizing Press Machine page describes compression molding of test specimens, with a working space whose upper part is heated and whose lower part is cooled, and it lists inspection of raw material for gel, black spots and stains among its uses. The Polytevo Series Vacuum Plate Vulcanizing Press page adds a fully enclosed vacuum hood and a program that sets vacuum pressure and the number of degassing cycles.
Pressing is also a topic in its own right on this site. The Laboratory Hot Pressing Guide covers heated platens and heated dies, vacuum and controlled atmosphere, platen size and the limits of a laboratory press, and it is the place to go when pressing, rather than the whole route, is the question. Cooling rate deserves a line of its own in the record: in semi-crystalline polymers it changes crystallinity,17 so a plaque cooled between platens and a plaque cooled in air may differ in crystallinity and in measured properties.
Choosing the shape from what the test needs
The shape should be chosen backwards, from the test. The table gives a typical match; the method reference for each test names the specimen it wants.
| If the test is | Then the shape is usually | Why |
|---|---|---|
| Tensile or other load test | Molded bars, or bars cut from a pressed or molded plate | The method defines the specimen; flow orientation affects the result |
| Impact | Molded bars, or bars cut from a plate, then notched if the method requires | Notch and preparation both change the energy absorbed |
| Melt flow | Pellets or chopped strand, no further shape | Further molding is unnecessary, but prior processing, drying and thermal history can still affect melt-flow results; retain those records |
| Heat deflection or Vicat | Bars or plaques from molding or pressing | Both tests need flat, uniform pieces of defined size |
| Hardness | A flat piece of sufficient thickness | The indentation needs a smooth surface and enough material beneath it |
| Filament, film or pipe use | The extruded form itself | The use is the test: diameter, thickness or wall, and the property of that form |
6. Stage 4, specimen: from a shape to a test piece
A test measures the specimen, not the material. Between a molded plate and a number on a screen there is a test piece with a geometry, a surface, a notch if any, and a condition, and each of those can move the result. The methods say so themselves: the standard test method for Izod impact lists the method of fabrication, the method and quality of the notch and the environment among the parameters that may affect the result significantly, and the standard tensile method treats specimen preparation as a topic of its own.18,19
Mold to size, mill, punch or cut
There are four ways to get a specimen. It can be molded to size, which is the route of the molding machines in the previous section. It can be milled out of a plate or sheet, which can give a smooth, accurately shaped edge in rigid and semi-rigid materials. It can be punched with a die, which suits rubber, film and flexible sheet. Or it can be cut with a die or knife. The tensile test method for molding and extrusion plastics accepts specimens that are molded to the chosen dimensions or machined, cut or punched from injection- or compression-molded plates, and it prefers a multipurpose specimen.20
Test method reference: ISO 527-2:2025.20
The Polytevo pages cover this ground as follows:
- Milling. The Polytevo Series Dumbbell Specimen Cutting Machine page describes milling of dumbbell and rectangular specimens from semi-rigid plastics and rigid non-metallic materials between molds with a milling cutter, supplied with a template for one dumbbell type; other specimen types need their own mold, confirmed on quotation.
- Manual punching. The Polytevo Series Manual Punching Machine page describes lever-operated and handwheel-operated machines that punch rubber, plastic, films, leather and other special materials into standard test pieces. The package is the machine with a nylon plate; the die for the test piece required is confirmed on quotation.
- Pneumatic punching. The Polytevo Series Pneumatic Punching Machine page describes machines that punch standard test pieces with compressed air, one of them with a safety light curtain and precision guide pillars. Dies are again not part of the package.
- Cutting dies. The Polytevo Series Specimen Cutting Dies page describes die options, dumbbell dies and tear dies, for preparing dumbbell and tear test specimens; the die and the machine it is used on are confirmed on quotation.
Which of these is right depends on the material and the shape. A punch or die generally suits thin, soft or flexible material; a mill generally suits stiffer plastic where an accurate, smooth edge matters. In both cases the tool is part of the specimen record, because a worn die or a dull cutter can leave a damaged edge, and a damaged edge can initiate failure.
Notching
Impact tests on plastics often use a notched bar. The notch is a deliberate stress concentration: it makes the bar fail at a known place and in a way that can be compared. Where the selected impact method specifies a notch, verify and record its prescribed geometry and preparation. The Izod method lists the method and quality of notching, the design of the notching apparatus and the time between notching and test among the parameters that may affect the result significantly,18 and the Charpy and Izod methods set their test parameters according to the type of notch.21,22
Notching is a machine step with its own record: the cutter type, the notch depth, the time between notching and test, and how many bars were notched in the same session. Unnotched bars are a different test, and a notched bar from a different notching setup is a different specimen.
The Polytevo Series Notching Machine page describes a manual and an automatic machine that cut the notch in plastic impact specimens for Izod and Charpy pendulum testing, with a standard notch cutter and further cutter types as options on the automatic machine.
Conditioning and the specimen record
Specimens are usually conditioned at a stated temperature and humidity for a stated time before testing. Use the conditioning or dry-state requirements of the applicable material specification and test method. Record the actual history. Moisture uptake can change the mechanical response of polyamides, so dry and conditioned specimens should not be compared as though their states were identical.23 The conditioning times and atmospheres belong to the test method reference, not to this guide, and the actual conditioning of the actual bars belongs in the record.
The specimen record is the fourth of the five: how the specimen was made (molded, milled, punched, cut), with which tool, the notch if any, how many specimens were prepared, the day they were prepared, and the conditioning. Where the specimens came from a plate, add where in the plate and in which direction relative to the flow, because that is the next topic.
Why specimen history changes the result
Specimens cut from the same plate along and across the flow direction are not equivalent, especially in filled and fiber-reinforced materials. In the study of short-glass-fiber-reinforced PBT mentioned above, the strength depended on the thickness of the layer in which fibers lay along the loading direction, and that thickness was strongly affected by the molding conditions and the gate position.14 The practical consequence is that a comparison needs one plan for where specimens are taken, applied to every material in it.
A tidy specimen record also makes a failed test informative, because the cause of an odd result can be looked up instead of guessed. The rule this guide repeats at every stage applies here too: prepare every specimen in a comparison the same way, and write the way down.
7. Stage 5, test: pick the property, then the instrument
The last stage is the one the other four exist to serve, and the order of choice is the point: decide which property the question needs, find the method reference that measures it, and only then look at instruments. The handbooks of plastics testing cover the field property by property, and the instrument is the means, not the aim.24,25,26 Each subsection below gives the idea of the test, what it can and cannot say, and the Polytevo page that describes the instrument.
Flow: MFR and MVR
The melt mass-flow rate (MFR) is the mass of polymer that flows through a standard die in a stated time under a stated temperature and load; the melt volume-flow rate (MVR) is the volume. Converting between them requires the melt density at the test conditions.27
Test method reference: ISO 1133-1:2022 and ASTM D1238-26.27,28 The shear rates in these methods are much smaller than those of normal processing, so values for different thermoplastics will not always correlate with their behavior in processing.27 A result at one temperature and load does not establish a full rheological flow curve or predict processing performance on its own; the melt rheology literature explains why: viscosity depends on shear rate, and one number cannot carry that dependence.29 The standard test method itself notes that melt flow rate is not a fundamental property and may not correlate with processing.28 Validated, material-specific correlations can nevertheless be useful.28,30 A review of the melt flow index describes it as more than a quality control number, discussing its correlations with processing and product behavior as well as its limits.30
Melt flow is not the same as processability, and a lab that reads it that way can be surprised in production. It is, however, one practical comparison of whether two lots, or a compound before and after a stage, differ in flow.
The Polytevo Series Melt Flow Indexer page describes instruments that measure MFR by the mass method and MVR by the volume method, in standard, automatic and motorized-weight-lifting configurations.
Heat: HDT and Vicat
Two simple tests give comparison temperatures for a plastic that is heated under load. In heat deflection temperature a bar under a bending load is heated at a steady rate until it deflects by a stated amount; in Vicat softening a flat-ended needle under a load is pressed into the surface while the sample is heated until it has penetrated by a stated amount. Test method reference: ISO 75-1:2020 and ASTM D648-18 for heat deflection, and ASTM D1525-25 for Vicat softening.31,32,33 Both are comparison numbers measured under fixed conditions; neither is a safe service temperature. Compare heat-deflection results only when the method, loading, specimen and thermal history are aligned; values obtained by different methods, including HDT and Vicat, should not be pooled as equivalent.
The Polytevo Series HDT and Vicat Softening Temperature Tester page describes equipment for heat deflection temperature and Vicat softening temperature testing.
Tensile and other load tests
A tensile test pulls a specimen at a controlled speed and records force and a method-appropriate deformation measurement, from which stiffness, yield, strength and elongation are read. Use the specimen cross-section to calculate stress and the specified reference length to calculate strain. Modulus and elongation require the deformation measurement prescribed by the selected method; crosshead travel is not automatically an adequate substitute.19,34 Test method reference: ISO 527-1:2019, ISO 527-2:2025 and ASTM D638-22.19,20,34 The result also depends on the speed, the temperature, and, as the previous section showed, on how the specimen was made. Select a force-measuring range and deformation-measurement method suitable for the expected test and the properties to be reported; capacity alone does not establish measurement accuracy.
The Polytevo Series Universal Testing Machine page describes tensile, compression, bending, shear, tear, peel and penetration testing of metallic and non-metallic materials, including plastics, with testing software and a set of tensile fixtures supplied as standard; other fixtures are optional.
To follow what happens when the same test is run at temperature, see In-Situ Tensile Testing at Variable Temperature.
Impact: Charpy and Izod
Pendulum impact tests release a swinging striker to impact a specimen and determine the absorbed energy under the selected method. In a Charpy test the bar lies supported at both ends and is struck in the middle; in an Izod test it is clamped as a cantilever and struck near the free end. Test method reference: ISO 179-1:2026 for Charpy and ISO 180:2023 for Izod, with ASTM D256-26 for Izod pendulum impact.18,21,22 Results are expressed as energy absorbed per unit of specimen width or per unit of cross-sectional area under the notch, depending on the method,18 so numbers should be compared only within one method. Record the failure category required by the method; do not treat different failure categories as directly comparable.18 The standard Izod method also cautions that the method of fabrication, the method and quality of the notch, the time between notching and test, and the environment can all change the result significantly.18
The Polytevo Series Charpy Impact Tester page describes a digital Charpy tester with selectable pendulum energy ranges, a touch screen and a built-in micro printer, for rigid plastics and other non-metallic materials, and it points to a separate Izod tester for Izod tests. The Polytevo Series Izod Impact Tester page describes the Izod tester, with its own set of pendulum energies and stored result groups.
Select the pendulum energy the method recommends for the expected result, and avoid the extremes of its range.
Hardness
Shore hardness is measured by pressing a spring-loaded indentor into the surface and reading a dial. Shore A suits softer materials and Shore D harder ones. For rubbers there is a theoretical relation between indentation hardness and Young’s modulus,35 but the durometer method itself calls its result an empirical number intended primarily for control purposes, with no simple relationship to a fundamental property.36 Test method reference: ASTM D2240-15(2021).36 Hardness can therefore serve as a screening number, best compared between specimens of the same kind measured the same way.
The Polytevo Series Shore Durometer page describes pointer-type Shore A and Shore D durometers, each with a constant-load test stand, for vulcanized rubber and plastic products.
Dispersion check
A compound can have the right formulation and still be poorly mixed. The filter pressure value test passes a compound of a color concentrate in a test polymer through an extruder with a melt pump and a screen pack, and reads the rise in pressure in front of the screen as undispersed particles load it. Test method reference: ISO 23900-5:2015.37 That standard states that the value is valid only for the equipment, conditions and test polymer used, and that results for different colorants are comparable only when the color concentrates were prepared the same way. A filter pressure test is also a stage-two check: it tells you about the compound before any specimen is made.
The Polytevo Series Filter Pressure Value Tester page describes an extruder with a gear-type melt pump, a screen pack assembly and melt temperature and pressure sensors, for quantifying the dispersion quality of pigments and fillers in polyolefin and other thermoplastic compounds, with test data exported with analysis charts; it states that a higher value indicates poorer dispersion.
Reading a result honestly
A result is only as good as its conditions and its spread. Report the method reference, the instrument and its range, the conditions, the number of specimens and the spread between them, not just a mean. The number of specimens is set by the method reference and not by a rule of thumb in this guide. Differences in material history, specimen preparation, conditioning, test conditions or the measurement system can contribute to disagreement. Compare those conditions and their records before assigning a cause. The five records in section 10 list the conditions to compare: the resin lot and drying, the compounding history, the molding conditions, the specimen preparation, and the test conditions.
8. The Polytevo equipment table: all 31 pages by stage
This is the one table in the guide that names every machine. Each row links the live page of one Polytevo Series by ACS Material product, places it in the stage where it is used, and gives its role in a few words taken from what the page says. It carries no specification numbers on purpose: numbers are published on the product pages, they are updated there, and a table of them here would go out of date.
Counts by stage: material 2, compound 8, shape 9, specimen 5, test 7, which makes 31 pages. A few machines span two stages. The extruders and the two-roll mill sit in compound even though some also produce an extrudate, and the filter pressure value tester sits in test because it is a quality check on a compound. Where a page lists more than one model, the roles in the table are those of the page, and model-specific details stay on the page.
Jump to a stage: Material | Compound | Shape | Specimen | Test
| Stage | Polytevo Series page | Role in the route |
|---|---|---|
| Material | Laboratory Plastic Shredder ACS-7002 | Crushes hard-plastic sprue and runner scrap from injection molding in small laboratory batches |
| Material | High Speed Mixer ACS-1001 | Mixes and colors resin and pellets before processing |
| Compound | Single Screw Extruder ACS-7008 | Mixes and processes polymers and masterbatch; supplied with a cooling tank and an air-drying and pelletizing unit |
| Compound | Benchtop Single-Screw Extruder ACS-7008B16 | Benchtop single-screw extruder for teaching demonstrations and small-batch extrusion |
| Compound | Benchtop Mini Extruder ACS-7103E | Benchtop extrusion system for compounding new materials and making small-batch extruded specimens |
| Compound | Recirculating Single-Screw Extruder ACS-7008ZM | Circulating flow channel and reversing valve for laboratory mixing, plasticization and extrusion |
| Compound | Conical Twin-Screw Extruder ACS-7009ZS | Conical twin-screw extruder for micro-sample blending of new or costly materials |
| Compound | Dual Conical Twin-Screw Extruder ACS-7009ZSD | Conical twin-screw sets with independently adjustable speeds for micro-sample blending of highly filled and high-viscosity materials |
| Compound | Twin-Screw Extrusion and Pelletizing Line ACS-7009P-20B | Co-rotating twin-screw compounding with strand pelletizing for PE and PP formulations |
| Compound | Two-Roll Mill ACS-7007-120 / ACS-7007-150 | Heated rolls for plasticating, mixing and dispersion of polymers |
| Shape | Single-Screw Pipe Extrusion Line ACS-7008D | Small-diameter pipe with vacuum sizing, haul-off and cutter |
| Shape | 3D Printing Filament Extrusion Line ACS-7008DP | 3D printing filament with laser diameter measurement and automatic winding |
| Shape | Fiber-Core 3D Printing Filament Coating Line ACS-7008DPC | Coats continuous fiber cores with thermoplastic to make fiber-core 3D printing filament |
| Shape | Cast Film Extrusion Line ACS-7008LY | Cast film forming experiments, including dispersion testing of color masterbatches |
| Shape | Film Blowing Machine ACS-7008FB | Blown film; film-blowing feasibility and internal gel content |
| Shape | Precision Injection Molding Machine ACS-7003 | Injection molding of test specimens; pneumatic ACS-7003 and hydraulic ACS-7003H |
| Shape | Vertical Transfer Molding Machine ACS-7003YZ | Transfer molding of standard specimens: tensile, flexural, impact and color plaque |
| Shape | Plate Vulcanizing Press Machine ACS-7006A | Platen press for compression molding of test specimens |
| Shape | Vacuum Plate Vulcanizing Press ACS-7006ZGI | Plate press with a vacuum hood for sheeting and sample preparation |
| Specimen | Manual Punching Machine ACS-4025L and ACS-4025H | Manual punching of rubber, plastic, film and leather into standard test pieces |
| Specimen | Pneumatic Punching Machine ACS-4025P and ACS-4025D | Compressed-air punching of standard test pieces |
| Specimen | Dumbbell Specimen Cutting Machine ACS-5002 | Mills dumbbell and rectangular specimens from semi-rigid plastics and rigid non-metallic materials |
| Specimen | Notching Machine ACS-5001 / 5001A | Cuts the notch in impact specimens for Izod and Charpy testing |
| Specimen | Specimen Cutting Dies ACS-CD | Cutting dies for dumbbell and tear test specimens |
| Test | Charpy Impact Tester ACS-4020 | Charpy impact of rigid plastics and other non-metallic materials |
| Test | Izod Impact Tester ACS-4021 | Izod impact toughness of plastics and other non-metallic materials |
| Test | Melt Flow Indexer ACS-5005, 5005A, 5005SA | Melt mass-flow rate (MFR) and melt volume-flow rate (MVR) |
| Test | HDT and Vicat Softening Temperature Tester ACS-5006-TC3 | Heat deflection temperature (HDT) and Vicat softening temperature |
| Test | Universal Testing Machine ACS-8000A | Tensile, compression, bending, shear, tear, peel and penetration testing |
| Test | Shore Durometer ACS-LX-A and ACS-LX-D | Shore A and Shore D hardness of rubber and plastic products |
| Test | Filter Pressure Value Tester ACS-7008FPV | Filter pressure value test of pigment and filler dispersion in thermoplastic compounds |
Product statements in the table are those of the live pages on 15 November 2026. Specifications and configurations are as published on each page, and final configurations are confirmed on quotation.
9. Two worked routes
The two routes below are illustrations of how the five stages connect, not recipes and not results. They contain no data. Their purpose is to show which record is kept where.
Route A: a new filler in a polyolefin
The question is whether a new filler changes the stiffness, impact behavior and flow of a polyolefin. The route has a control from the first stage: the unfilled polymer goes through every stage in the same way, because only the difference between the two is meaningful.
- Material. Record the polymer lot and the filler lot, the drying state of each, and the composition by mass of each blend. Pre-blend the dry components in the high speed mixer if the blend is to be fed as a mixture, and record this as a pre-blending operation, without treating it as evidence of final dispersion.
- Compound. Run the control and the filled blend on the same compounding machine with the same set-up, for example a conical twin-screw machine for a small quantity or the twin-screw line for a larger one. Record the temperatures, speeds and the time in the machine, and the torque trace if the machine provides one.
- Shape. Choose one shaping route for both materials, a pressed plaque or molded bars, and do not change it halfway through. Record the tool temperatures, the pressure or injection conditions and the cooling.
- Specimen. Mill, punch or cut the same specimen type from the same place in each plaque, notch the impact bars with one notcher setup, and condition all specimens together.
- Test. Tensile on the universal testing machine, impact on the Charpy or the Izod tester, melt flow on the indexer, each under the conditions named by its method reference. When comparing filled and unfilled materials, consider density differences rather than attributing every change in MFR to viscosity. Record the number of specimens and report the spread.
The result is a comparison of two materials through one route. It says nothing about how the filler would behave at production scale, and it should be written that way.
Route B: regrind into filament
The question is whether regrind from molding sprues and runners can be made into filament that prints a usable test bar. Here the route is a chain and each stage hands over a physical object.
- Material. Shred hard-plastic sprue and runner scrap in the laboratory plastic shredder, record the source, the screen used and the drying state, and keep the regrind lot separate from any virgin material.
- Compound. If a colorant or additive is needed, blend it with the regrind before extrusion and record its amount by mass.
- Shape. Extrude on the filament line and record the temperatures and the speeds. Read the diameter measurement along the length and keep the log, because the variation of diameter is the first result of the route.
- Specimen. Print the test bars on your own printer with fixed settings, and record those settings, since the printing process has its own large effect on strength.
- Test. Pull the printed bars in tension and report the specimen count and spread. The record from each earlier stage travels with the result.
Both routes use the same discipline, which is the point of the guide: every stage has a written record, every comparison uses one route, and the result states the route it came from.
10. The route record: what to write down at each stage
The record is one table with one row per stage. It can be a printed form at the bench or a spreadsheet; what matters is that it is filled in as the work happens, not afterwards. The fields below help document and investigate differences between results.
| Stage | Fields to fill in |
|---|---|
| Material | Resin and lot; form (pellet, powder, regrind, film scrap); size reduction and screen used; drying state; additive or filler and its lot; composition by mass; source of any regrind |
| Compound | Machine and set-up; formulation by mass; temperature profile and melt temperature if read; speed and feed rate; time in the machine or number of cycles; roll gap and passes for a mill; torque trace if available |
| Shape | Forming route; melt temperature; tool or platen temperature; pressure, injection or haul-off conditions; cooling method and time; diameter or thickness log for filament and film; flow direction |
| Specimen | How it was made: molded, milled, punched or cut; tool and its condition; position and direction in the plate; notch type, depth, radius, orientation, preparation date and inspection record; number prepared; conditioning |
| Test | Method reference and instrument; range or load; temperature and speed; number of specimens; spread; date; operator |
11. The Polytevo knowledge hub
This guide is the entry point to the ACS Material library on lab-scale polymer processing and testing, built around the Polytevo Series by ACS Material. The eight areas below are planned guides, each of which goes deeper on one part of the route; they are listed here as plain text and will be linked as they are published.
- Lab extruders. How to choose a laboratory extruder: screw type, batch size, and what each type is for.
- Mechanical and hardness testing. Match the test to the question: tensile, impact and hardness.
- Melt flow and heat tests. Reading a datasheet: what melt flow rate, heat deflection and Vicat softening tell you.
- Molding test specimens. Injection, transfer and compression molding of test bars and plaques.
- Specimen preparation. Cut, punch, mill and notch: how to prepare a specimen that tests the material.
- Extrusion lines and output forms. Pipe, filament, cast film and blown film: what each line produces.
- Compounding and material preparation. Shredding, pre-blending and compounding before the first specimen.
- Dispersion and quality control. How to check that a filler or pigment is dispersed, and what to do when it is not.
12. Before you request a quote
To help identify a suitable configuration, describe the route and the measurements you need. Please tell us:
- the material and its form, for example pellets, powder or regrind, and the polymer family;
- the batch size you need to work with at each stage;
- the shape you want out of the machine, for example strand, film, filament, plate or molded bar;
- the test you need to run, and the method reference you work to;
- the specimen type, and whether you also need cutting dies or a notching step.
Send these through Request a Quote. Specifications are as published on each product page, and final configurations are confirmed on quotation.
13. FAQ
What does “lab-scale” mean for polymer processing?
Working with grams to a few kilograms of material on a bench machine to learn how a material behaves, as opposed to producing goods. It is a working judgment rather than a standard, and a lab-scale result describes the material on that machine under those conditions.
Do I need to compound before I can test a material?
Not necessarily. A received compound or specimen may be tested without further compounding. Include a mixing or compounding operation when it is needed to prepare the formulation being investigated, and document that operation.
Can I test directly from an extruded strand?
For some uses. A strand can be chopped or pelletized and fed to a melt flow test, and the diameter of a filament can be measured directly. Mechanical tests need a specimen of defined geometry, so a strand is usually shaped further first, unless the method names a strand specimen.
Why do two labs get different numbers from the same resin?
Differences in material history, specimen preparation, conditioning, test conditions or the measurement system can contribute to disagreement. Compare those conditions and their records before assigning a cause; section 10 lists the fields to document.
Which comes first, choosing the machine or choosing the test?
The test. Decide the property the question needs, find the method reference for it, and let the method decide the specimen, the shape and then the machines that can produce them.
Is melt flow rate the same as processability?
No. Melt flow rate is a single point measured under fixed conditions, and the standard method itself notes that it may not correlate with processing. It can support comparisons under specified conditions, but a processing prediction requires a validated relationship for the material and process being considered.28
How many specimens should a lab prepare?
The method reference for the test decides. Prepare at least the number it names, and report the spread between specimens rather than only the mean.
What should I record so a result can be repeated?
The five records in section 10: the material, the compound conditions, the shape conditions, the specimen preparation and the test conditions, together with the method reference.